The Hidden Cost of Post-Processing in Additive Manufacturing
The brochure version of additive manufacturing is seductive: a digital file becomes a flight-ready bracket overnight, with no tooling, no fixturing, no six-week lead time. What the brochure omits is what happens after the build plate cools - and that omission has quietly become one of the most expensive assumptions in American defense manufacturing.
Post-processing in metal additive manufacturing is not a footnote. For programs operating under AS9100 or NADCAP certification requirements, it is frequently the dominant cost center, the primary schedule risk, and the variable most likely to invalidate the business case that got the program funded in the first place. Operations directors who inherited additive capacity from an enthusiastic engineering team are learning this the hard way.
What "Post-Processing" Actually Means at Scale
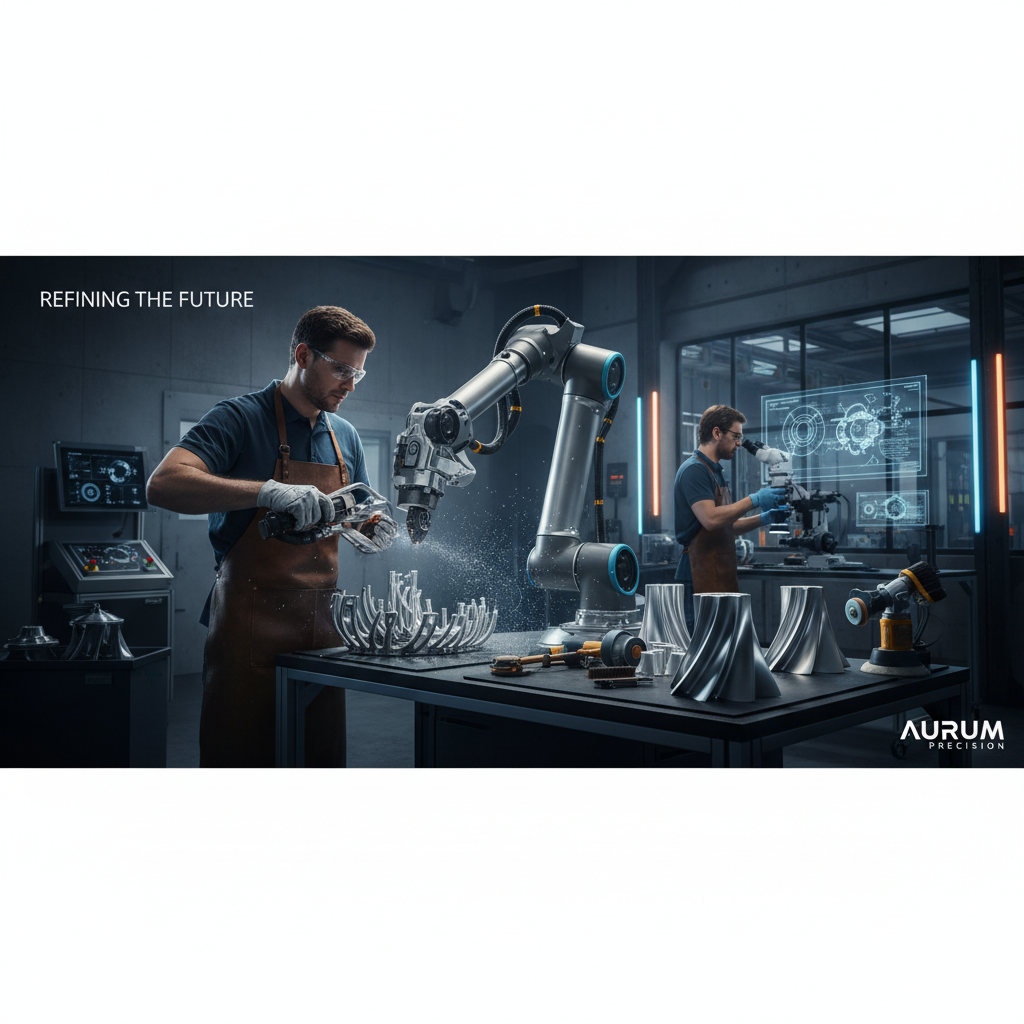
The term itself is dangerously vague, which is part of the problem. In practice, post-processing for metal parts produced via laser powder bed fusion (LPBF) or directed energy deposition (DED) encompasses a chain of operations that can rival traditional subtractive machining in both time and cost:
- Stress relief and heat treatment - mandatory for most structural aerospace applications, requiring furnace cycles that can run eight to twelve hours per batch
- Support structure removal - a labor-intensive operation that, for complex internal geometries, may require EDM wire cutting, hand grinding, or specialized fixtures that defeat the "no tooling" narrative
- Hot isostatic pressing (HIP) - standard practice for flight-critical components to close internal porosity, requiring external service bureaus for most in-house additive operations
- CNC finish machining - because as-built surface finishes from most powder bed systems remain incompatible with tight-tolerance mating interfaces
- Non-destructive testing (NDT) - CT scanning, fluorescent penetrant inspection, and ultrasonic testing requirements that are more demanding, not less, for additively manufactured parts entering certified supply chains
Each of these steps introduces queue time, handling risk, and in many cases, third-party dependencies. The geometry freedom that additive promises on the front end frequently creates inspection and finishing complexity that conventional machining simply does not. A turbine housing with internal conformal cooling channels - the canonical additive success story - still needs those channels cleaned of unsintered powder, verified free of blockage, and pressure-tested before it goes anywhere near a hot section.
The HIP Problem Nobody Talks About Loudly
Of the post-processing steps listed above, hot isostatic pressing deserves particular attention because its constraints are structural, not merely operational. The United States has a limited number of qualified HIP service providers capable of processing aerospace-grade titanium and nickel superalloys under the cycle conditions required by OEM and prime contractor specifications. Quintus Technologies, Bodycote, and a small cohort of specialized shops represent the functional capacity ceiling for much of the industry.
For defense primes scaling additive production - whether for the F-35 sustainment supply chain, next-generation rotorcraft components, or hypersonic vehicle structures - this bottleneck is not theoretical. Programs that model their throughput around additive's speed advantage frequently discover that HIP queue times of several weeks per batch compress or eliminate whatever schedule benefit the build process created. The Pentagon's broader push to modernize the defense industrial base, reflected in initiatives under the Office of Industrial Base Policy, has begun to surface this constraint explicitly. Capital investment in HIP capacity is a defense manufacturing problem, not just an additive manufacturing problem.
The Labor Equation Doesn't Disappear
One of the more persistent myths surrounding additive manufacturing is that it reduces skilled labor requirements. In aerospace and defense applications, the opposite is frequently true - or more precisely, it trades one category of skilled labor for another that is harder to find and more expensive to certify.
Support removal from complex titanium builds requires operators who understand metallurgy well enough not to introduce stress risers or surface damage during mechanical operations. Powder handling and recycling protocols under OSHA and internal safety standards require trained personnel with documented procedures - reactive metal powders are not a casual handling matter, as several facility incidents across the industry have demonstrated. Post-build inspection for additive parts, particularly those with internal features inaccessible to conventional probing, requires NDT technicians with CT interpretation skills that remain scarce in the broader manufacturing workforce.

What will it take to turn demand into delivered output?
Explore The Capacity Imperative, our report on U.S. advanced manufacturing and the priorities shaping 2027.
Lockheed Martin, Raytheon, and GE Aerospace have all made substantial investments in additive centers of excellence precisely because centralizing this expertise is more tractable than distributing it. For tier-two and tier-three suppliers being pressed to adopt additive by their prime customers, the labor and certification burden of standing up a compliant post-processing operation is a legitimate barrier - one that doesn't appear in the ROI models that justified the printer purchase.
Design for Additive Manufacturing Means Design for Post-Processing
The engineering community has largely internalized design for additive manufacturing (DfAM) as a discipline, but the more operationally honest framing is design for the complete production system, including every downstream step. A component optimized purely for build efficiency - minimal supports, maximum geometric complexity, tight internal channel networks - may be a post-processing nightmare that consumes the time savings three times over.
This is where the gap between additive's early adopters and its mature practitioners becomes visible. Companies like Honeywell Aerospace and Arcam-equipped producers in the orthopedic and aerospace space have developed component design standards that explicitly account for support accessibility, post-machining datum availability, and NDT inspectability. These are not engineering elegance constraints; they are production system constraints that determine whether a part can be manufactured at cost and on schedule at volume.
The defense programs most successfully integrating additive - including elements of the Army's aviation sustainment work and Air Force depot-level repair initiatives - share a common characteristic: they treat post-processing as a first-order design constraint, not an afterthought managed by the manufacturing team after the design is frozen.
The Accounting Problem
None of this would be quite so consequential if cost accounting systems captured it accurately. They frequently do not. Activity-based costing for additive manufacturing remains underdeveloped at most facilities, particularly those that stood up additive capacity as an engineering function before it transitioned to a production function. Build machine time is tracked. Post-processing labor is often allocated to general overhead. HIP and external finishing costs are booked as purchased services without being tied back to part-level cost models.
The result is a systematic understatement of additive part cost that distorts make-versus-buy decisions, misrepresents program margins, and creates organizational incentives to keep printing parts whose true cost would not survive scrutiny. For publicly traded defense contractors, this is an internal controls issue as much as an operational one. For smaller manufacturers, it is the kind of accounting fog that precedes a painful reckoning when contract renewals force accurate cost disclosure.
Operations directors who want to lead rather than react on this issue need cost systems that capture post-processing at the part level, including allocated queue time at external service providers. The data exists. The discipline to collect and use it is less common.
The Path Forward Is Not Pessimism
Nothing in the above is an argument against additive manufacturing in defense and aerospace applications. The technology's genuine advantages - geometric freedom, part consolidation, rapid iteration, reduced material waste for expensive alloys, and distributed manufacturing potential - are real and strategically significant. The Air Force's successful use of additively manufactured components across legacy platform sustainment is documented. The Navy's interest in shipboard additive for at-sea repair has legitimate operational logic.
The argument is for operational honesty. Post-processing is not a problem that will be engineered away by the next generation of machines, though improvements in as-built surface finish and residual stress management are incremental positives. It is a permanent feature of the production system that demands the same rigorous planning, investment, and cost visibility as any other manufacturing operation.
The manufacturers who will build durable competitive advantage in defense additive are not those who print the fastest. They are those who have built post-processing infrastructure, labor capability, and cost accounting discipline that make the entire system - from digital file to certified part - predictable, traceable, and honest. Everything else is a brochure.

